Date: 2026-11-10 hits: 108
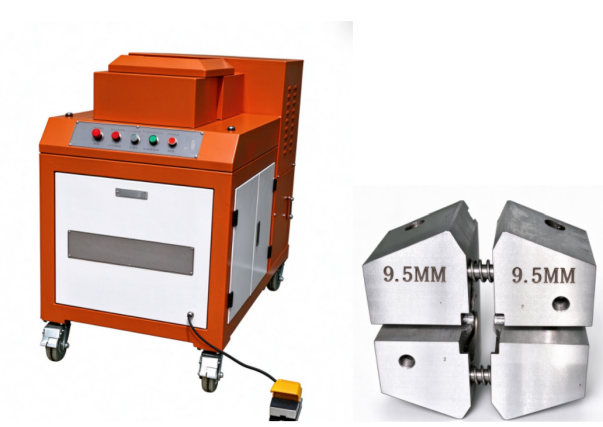
Desktop Manual Cold Welding Machine (Cold Pressure Welder) Working principle: Cold pressure welding is a solid-state welding process. No electricity, heating or filler metal is required. Under mechanical compression, the metal molecules on the contact surface of non-ferrous wires (copper, aluminum, gold, silver, nickel, etc.) are squeezed and combined to realize wire butt joint. It can weld silver wire, nickel wire and other non-ferrous metal wires. The welded joint features stable resistance and good tensile strength.
Application Scope
1.Industries: Wire & cable factories, wire drawing factories, enameled wire factories, precious metal processing
2.Weldable materials: Pure copper wire, pure aluminum wire, silver wire, gold wire, nickel wire and other non-ferrous metals with good plasticity
3.Functions: Butt joint for broken wire during wire drawing, wire splicing for stranding process, enameled wire connection, fine precious metal wire joint
4.Advantages: The joint has low resistance, stable conductivity and high tensile strength. No high-temperature annealing, so the joint will not become brittle as soldering does
5.Limitations: Not suitable for steel, stainless steel and high-impurity alloys. Only same-metal welding (copper to copper, aluminum to aluminum; copper-aluminum dissimilar welding is not available)
四、Standard Operation Procedure
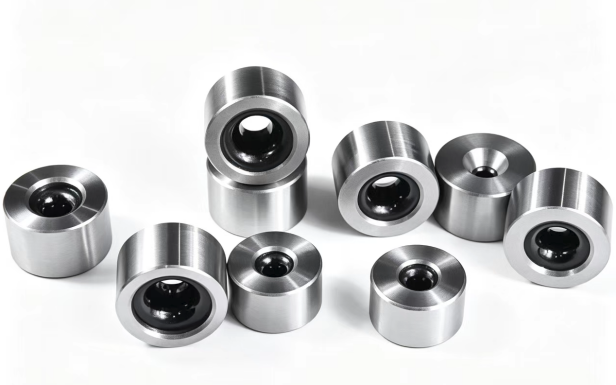
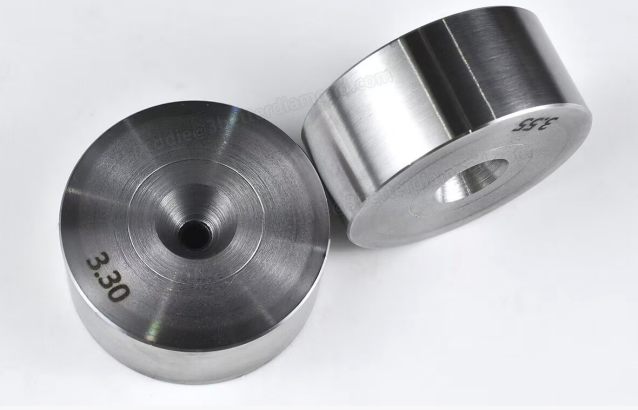
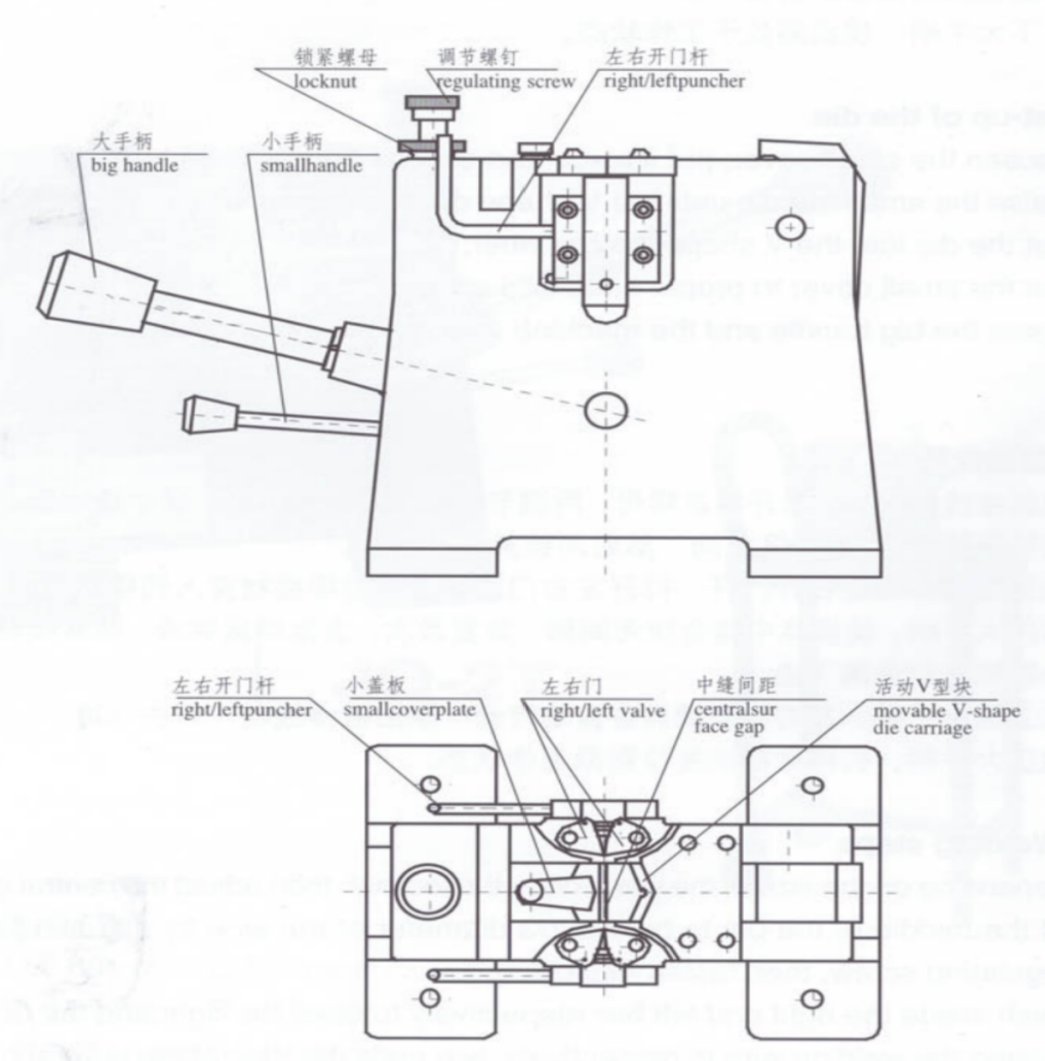
1.Select die & adjust gap: Choose the matching die according to wire diameter. Loosen the lock nut, adjust the limit screw, set the central gap of the die to 1/3 ~ 1/2 of the wire diameter, then lock the nut.
2.Clean wire ends: Remove enamel coating, oil contamination and oxide scale. Cut the wire ends flat. Dirt will cause weak joints and easy breakage.
3.Open die, feed and align wires: Pull the opening handle to open the die cavity. Insert two wires from left and right holes respectively, make the two wire ends butt tightly at the center of the die.
4.Cold welding by pressing: Press down the main handle firmly, squeeze repeatedly 2~4 times (more times for fine wire). Metal flash will extrude from the parting line during compression.
5.Take out wire & trim joint: Open the handle and take out the wire. Cut or grind off the outer flash on the joint. Pull gently to check the connection strength.
6.Reset: Release the main handle, the die rebounds and gets ready for next welding.
五、 Precautions
1.Wire requirement: Only same-type high-purity soft metal is allowed. Wire ends must be clean. Oil, enamel and oxide layer are the most common causes of cold welding failure. Enameled wire must be completely stripped of enamel.
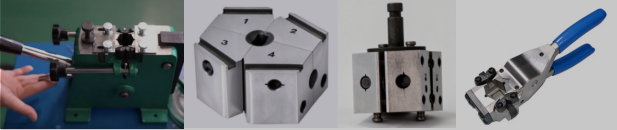
2.Die maintenance: Dies are wearing parts. Worn die cavity will lead to easy fracture of joints. Dies for different wire diameters cannot be mixed. Keep dies clean and avoid impact.
3.Gap adjustment: Too large gap → insufficient compression, cold joint and easy breakage. Too small gap → excessive metal extrusion, severely flattened joint, reduced tensile strength.
4.Safety: Do not place your hands at the die closing seam when pressing the handle. The lever force is strong to avoid pinch injury.
5.Machine maintenance: Apply a small amount of lubricating oil to rotating shafts and sliding parts regularly. Clean and anti-rust the dies if the machine is out of service for a long time.
6.Joint inspection: Spot check tensile strength after welding. If joints keep breaking, check wire cleanliness, die gap and die wear first.
7.Misunderstanding reminder: This is NOT an electric spark cold welder. It cannot repair molds or castings, only for wire butt splicing.