Date: 2026-11-10 hits: 107
Manufacturing Process
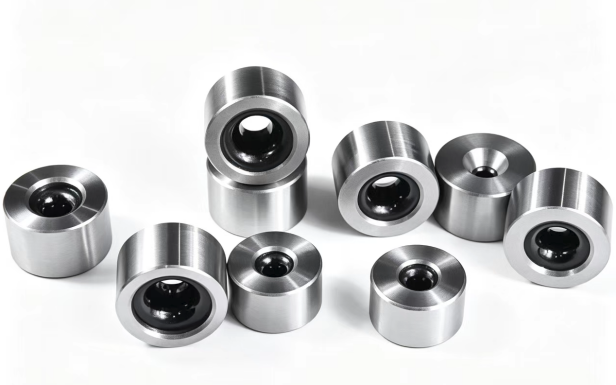
1. Blank selection & rough machining: Alloy steel / YG tungsten carbide blanks are selected according to working condition. Rough turning for core tip and die sleeve, leaving finishing allowance.
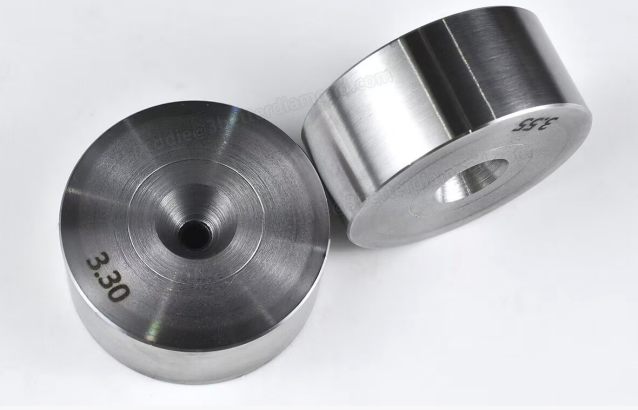
2. Precision finishing: CNC turning & boring to machine die sleeve inner bore and core tip outer taper, ensuring precise taper fit and smooth flow channel.
3. Lapping & polishing: Lap and polish runner and working surface contacting molten plastic to reduce roughness, prevent material sticking and carbon buildup.
4. Mating & fitting adjustment: Assemble core tip and die sleeve in pairs, check concentricity and extrusion gap for uniform outlet clearance.
5. Optional surface treatment: Hard chrome plating, nitriding, CVD / PVD coating to improve wear resistance, corrosion resistance and anti-plastic sticking property.
6. Cleaning, full inspection, marking & warehousing,inspect dimension, concentricity and surface finish, remove oil & debris, warehouse after passing inspection.
Main Advantages
1. Precise mating of core tip & die sleeve delivers uniform insulation / sheath wall thickness with low eccentricity, saving plastic raw materials and stable cable electrical performance.
2. Smooth runner enables fluent molten plastic flow, reduces stagnant & burnt material, minimizing defects such as particles, bubbles, scratches and burnt spots.
3. Good wear & corrosion resistance against filler abrasion, extending die life and cutting downtime.
4. Standardized design for easy specification change & machine setup, improving extruder productivity.
5. Smooth extruded cable surface with few pits, good finished appearance quality.